PLC programming
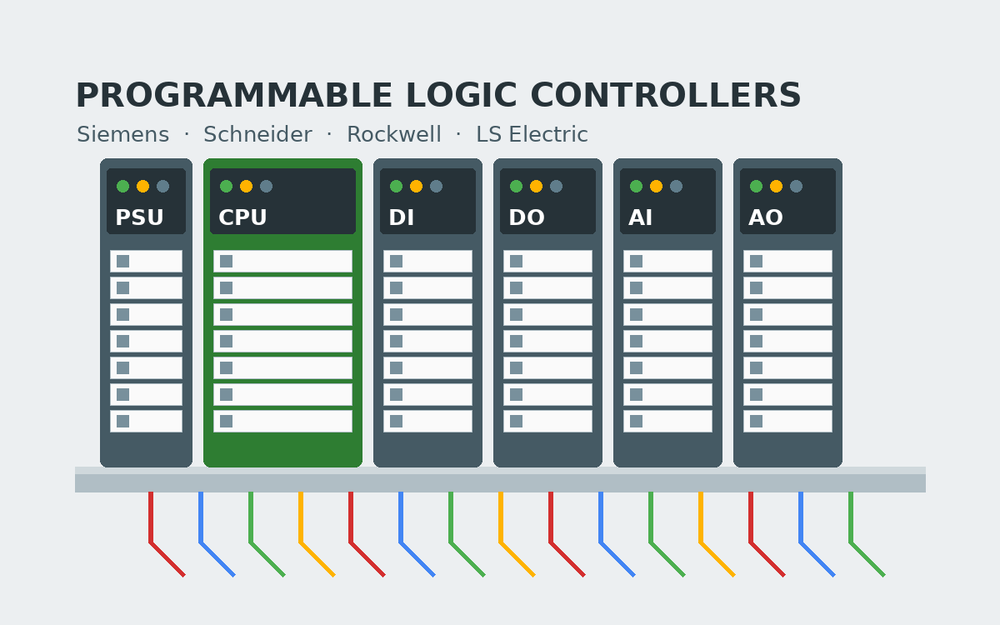
New logic, migrations, and rescue of undocumented legacy code across all four major platforms.
FHI designs, programs and supports PLC, SCADA and machine control across mining, manufacturing, pharmaceutical and process plants — from panel to historian, on site or remote.
Six things, done properly, rather than a catalogue of everything.
New logic, migrations, and rescue of undocumented legacy code across all four major platforms.
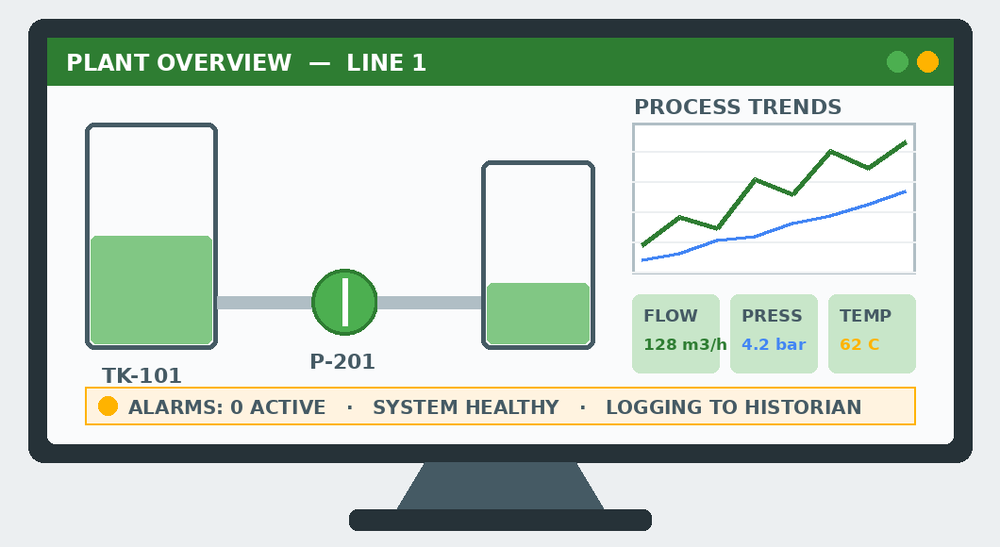
Operator screens built around the task — clear navigation, alarms that mean something, workable recipe handling.
Ignition, AVEVA and WinCC applications with historian logging, trending and shift reporting.
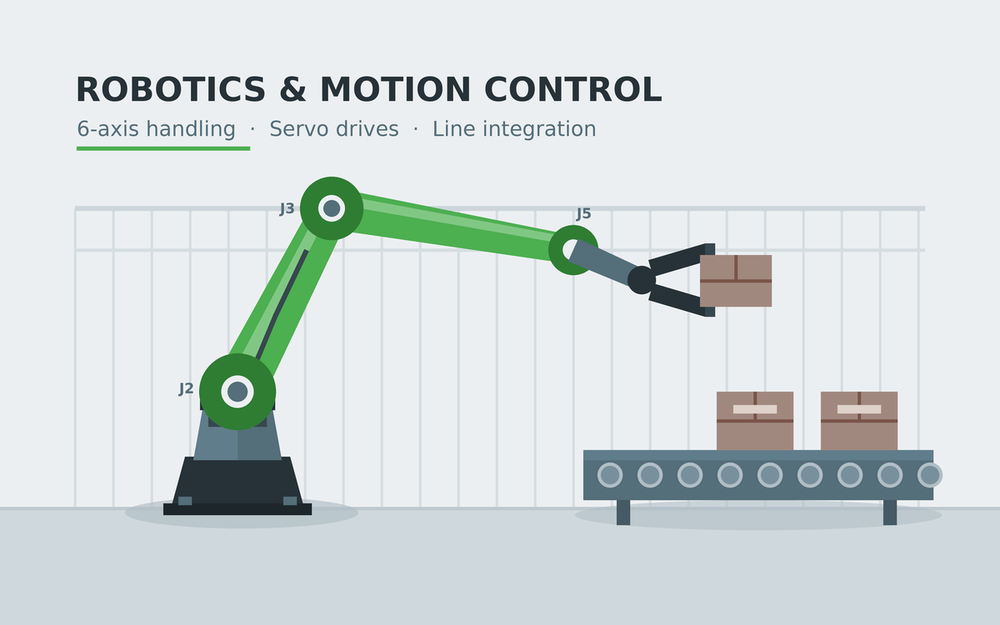
Full machine control: sequencing, servo and VFD motion, safety interlocks, and commissioning on site.
Breakdown response, fault diagnosis, drive and panel repair, and preventive review before the next stoppage.
PLC-to-PLC and PLC-to-MES links over PROFIBUS, EtherNet/IP, Modbus and OPC UA, into SQL and IIoT.
Vendor-agnostic in practice, not just on paper.
Client names withheld where confidentiality applies. References on request.
Campus-wide BMS for centralised monitoring and control of building services: HVAC and plant control, lighting and utility monitoring, alarm management, and a single supervisory interface for the estates team.
Siemens control system for an automated storage and retrieval system on a tyre production line. Stacker and conveyor sequencing, PLC-to-MES handshaking over PROFIBUS DP, recipe handling per press variant, and fault diagnostics on the curing line.
Drive migration and control logic rework on a QuantaSep buffer-maker skid. Rewritten motion layer, conductivity and pH control, and correction of buffer-step sequencing faults, with the IEC 61131-3 code reviewed against P&ID and instrument index.
Reactor and tank control with operator graphics and continuous historian logging of temperature, pressure, motor speed and tank weight, for batch traceability and shift reporting.
Source changeover and load management between solar, generator and grid supply, with generation, consumption and battery state monitored from a single SCADA interface.
Nine years inside plants before the consultancy, and it shows in the designs.
We work in the same conditions our clients do — remote sites, tight shutdown windows, and equipment that has to run. That means pragmatic designs, documentation you can actually use, and an engineer who answers the phone when a line goes down.
Send the machine, the platform and what it's doing wrong — or what you want it to do. You'll get an engineer's reply, not a sales sequence.